

For industrial manufacturing and laboratory research purposes only.
Product Specifications
| Parameter | Value |
|---|---|
| Model NO. | SGR-1503W |
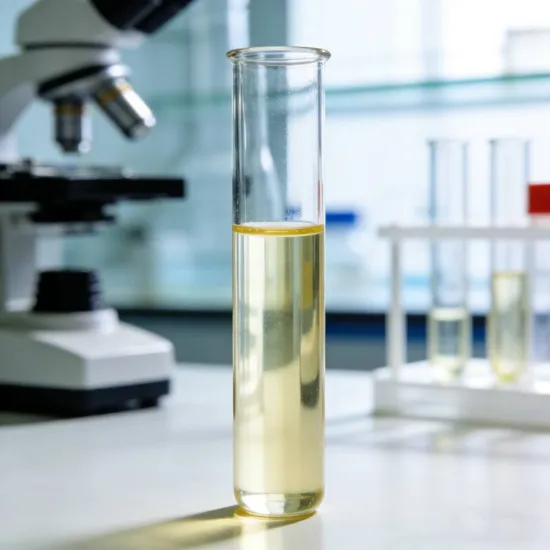
| Color | Light Yellow |
| Appearance | Liquid |
| Type | Reverse Osmosis (RO) Systems |
| Shelf Life | One Year |
| pH | 2.0-5.0 |
| Specific Gravity | ≥ 1.05 |
| Application | RO/NF/UF Systems |
| Transport Package | Blue Plastics Drum, White Plastics Drum |
| Specification | 25 kg/drum 1 ton/drum or as your requirement |
| Trademark | GIDINEW |
| Origin | Jining City, Shandong Province, China |
| Production Capacity | 5000ton/Year |
| Package Size | 120.00cm * 100.00cm * 115.00cm |
| Package Gross Weight | 1054.000kg |
Overcoming Scale Formation Challenges in RO/NF/UF Systems with Phosphate Free Scale Inhibitor
In our 10+ years serving industrial clients and research institutions, we've witnessed countless projects delayed by scale buildup in membrane systems. Traditional inhibitors often come with high minimum order quantities that strain R&D budgets, or contain phosphates that complicate wastewater treatment—especially problematic for startups and small-batch trial productions.
Phosphate Free Scale Inhibitor: Engineered for Efficiency and Compliance
Our Phosphate Free High Efficiency Scale Inhibitor addresses these pain points directly. As a fast-response chemical service provider, we specialize in small-batch orders, delivering within 7-15 days to keep your RO/NF/UF system maintenance on schedule. The phosphate-free formulation eliminates regulatory concerns associated with phosphorous discharge, making it ideal for both laboratory research and industrial-scale water treatment processes.
Industrial Applications Across Membrane Systems
This RO Scale Inhibitor is specifically designed for reverse osmosis (RO), nanofiltration (NF), and ultrafiltration (UF) systems—critical components in semiconductor manufacturing, pharmaceutical production, and research laboratories. Its high efficiency ensures continuous operation by preventing calcium carbonate, sulfate, and silica scale formation, which are common culprits in membrane fouling and pressure drop issues.
Key Specifications That Drive Performance
The liquid appearance (Light Yellow) allows for easy visual inspection and dosing accuracy, while the pH range of 2.0-5.0 ensures compatibility with most membrane materials. A specific gravity of ≥1.05 guarantees consistent concentration, eliminating the variability that can lead to under-dosing or over-treatment. With a one-year shelf life, researchers and plant managers can maintain inventory without frequent restocking, supporting long-term project continuity.
The Cost of Inadequate Scale Inhibition vs. Reliable Protection
Using substandard inhibitors risks membrane damage, increased energy consumption, and unplanned downtime—costs that far exceed the investment in quality chemicals. Our Phosphate Free RO Scale Inhibitor meets industrial standards for performance and safety, backed by a production capacity of 5000 tons/year to ensure supply stability even for growing operations. Clients report reduced cleaning frequencies and extended membrane lifespans, delivering measurable ROI within months of implementation.
Our commitment to quality is verified through rigorous batch testing, with each order accompanied by a Certificate of Analysis (COA). As a factory-direct supplier, we maintain full control over the production process, from raw material selection to final packaging in 25 kg or 1 ton drums. Our professional customer service team responds to technical inquiries within 24 hours, providing guidance on dosing rates and compatibility with existing water treatment chemicals.
Certificate of Analysis & Documentation
Every delivery includes a batch-specific COA and MSDS, ensuring full traceability and regulatory compliance. For research institutions requiring detailed performance data, additional test reports can be provided upon request, including efficacy studies under various operating conditions.
Storage & Handling
- Store in a cool, dry, well-ventilated area, sealed and away from direct sunlight.
- Keep away from incompatible materials, food and feed sources.
- Handle with appropriate personal protective equipment (gloves, goggles, lab coat).
- Follow good industrial hygiene practices. Avoid inhalation and skin contact.
- Refer to MSDS for detailed storage and safety instructions.
Streamlined Ordering for Laboratory and Industrial Needs
To request a quotation, simply contact our sales team with your required volume and delivery timeline. We offer flexible packaging options to suit small-batch research (25 kg drums) or larger industrial applications (1 ton drums), with no excessive minimum order quantities. Sample evaluations are available for qualified buyers to verify performance before full-scale procurement.
Frequently Asked Questions
Q: What is the shelf life of this scale inhibitor?
A: The product has a shelf life of one year when stored properly in sealed containers away from direct sunlight and extreme temperatures.
Q: Can this inhibitor be used in food or pharmaceutical production facilities?
A: This product is for industrial and laboratory research use only. It is not intended for direct contact with food, pharmaceuticals, or household applications.
Q: What documentation is provided with each order?
A: Each delivery includes a Certificate of Analysis (COA) and Material Safety Data Sheet (MSDS) specific to the batch.
Q: Do you offer custom packaging options?
A: Yes, we can accommodate custom packaging requirements beyond the standard 25 kg and 1 ton drums. Please specify your needs during the quotation process.
Q: How is the effectiveness of the scale inhibitor determined?
A: Effectiveness is verified through standard industry tests measuring calcium carbonate inhibition efficiency and compatibility with RO/NF/UF membranes, with results provided in the COA.