Inibidor de corrosão e antiescalante à base de fosfonato orgânico para o tratamento de água de circulação industrial

Inibidor de corrosão e antiescalante à base de fosfonato orgânico para o tratamento de água de circulação industrial

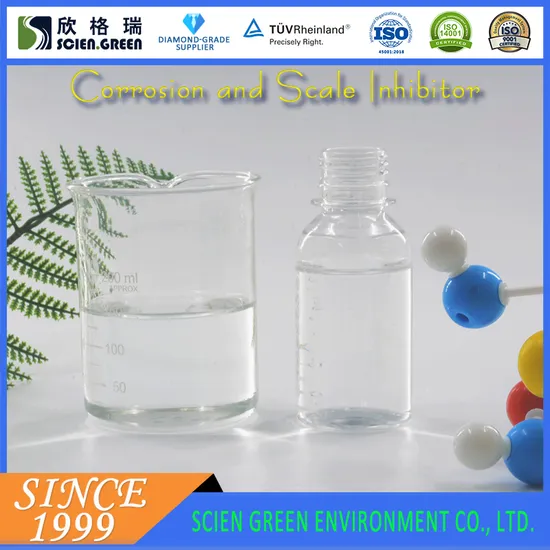
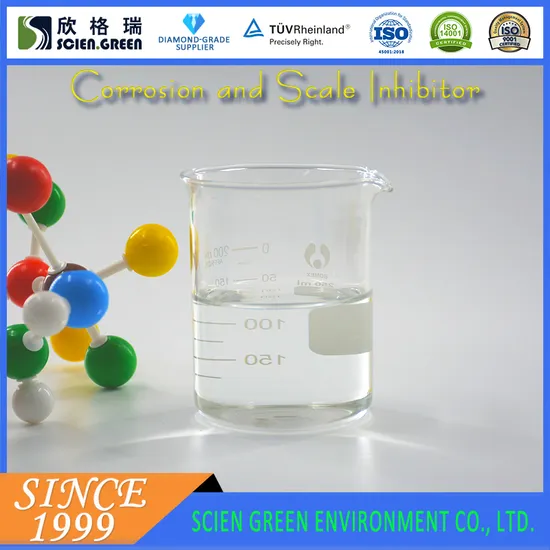
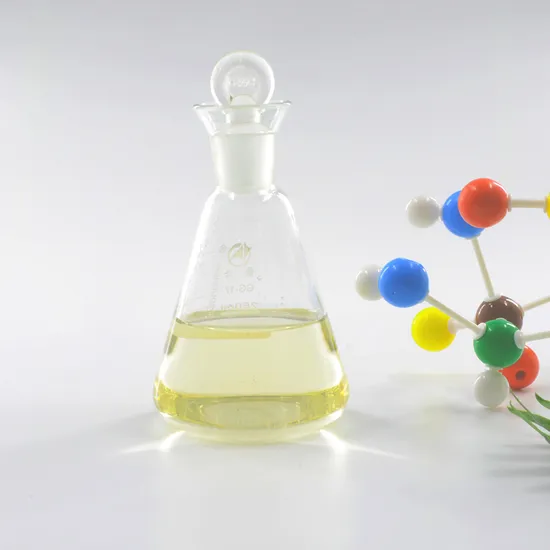
Keep industrial circulating water systems running efficiently with our Organic Phosphonate Scale Antiscalant Corrosion Inhibitor, designed to prevent scale buildup and corrosion that can disrupt operations. Ideal for R&D labs and small-batch trial production, this liquid solution (pale yellow to brownish yellow) delivers reliable performance with an organic phosphonate content (as PO₄³⁻) of ≥6.8%, ensuring effective inhibition even in demanding conditions.

  • Fast-acting formula maintains system integrity, reducing downtime and supporting timely project milestones
  • Flexible small-batch availability meets your specific needs without excess inventory
  • Stable pH (≤4.5 in 1% solution) and density (≥1.05 g/cm³ at 20°C) ensure consistent application results
Quality Certified
Technical Support
Custom R&D

Product Details

FOR INDUSTRIAL AND LABORATORY RESEARCH USE ONLY. NOT FOR DIRECT HUMAN CONSUMPTION, THERAPEUTIC OR HOUSEHOLD USE.
For industrial manufacturing and laboratory research purposes only.

Product Specifications

Parameter Value
Color Pale Yellow or Brownish Yellow
Appearance Liquid
Type Industrial Circulating Water Treatment Agent
Product Name Organic Phosphonate Scale Corrosion Inhibitor
Density (20°C) G/Cm³ ≥1.05
pH (1% Aqueous Solution) ≤4.5
Organic Phosphonate Content (as Po43-) % ≥6.8
Shelf Life 1 Year
Transport Package Blue / White Plastics Drum
Specification 25 kg/200 kg/1 ton drum
Trademark GIDINEW
Origin Jining City, Shandong Province, China
Production Capacity 15000 Ton/Year
Package Size 120.00cm * 100.00cm * 115.00cm
Package Gross Weight 1057.000kg

Addressing Scale and Corrosion Challenges in Industrial Circulating Water Systems

In industrial water management, inconsistent inhibitor performance often leads to unexpected equipment scaling, while delayed small-batch deliveries disrupt research timelines. Our 10+ years serving manufacturing plants and R&D labs across 50+ countries have shown that traditional suppliers' rigid MOQ requirements force customers into overstocking, tying up capital in unused inventory.

Organic Phosphonate Scale Antiscalant: Engineered for Reliable Water Treatment

Our Organic Phosphonate Scale Antiscalant Corrosion Inhibitor delivers consistent performance by maintaining strict quality control over key parameters like organic phosphonate content (≥6.8%) and pH stability (≤4.5 in 1% solution). Designed to address the "small batches, fast delivery" demands highlighted in modern industrial water treatment, this inhibitor supports both pilot-scale trials and emergency maintenance needs with 7-15 day turnaround for custom orders.

Industrial Applications and Treatment Efficacy

This Circulating Water Inhibitor is specifically formulated for closed-loop cooling systems, heat exchangers, and process water pipelines in chemical, power, and manufacturing industries. Its dual-action formula prevents calcium carbonate and phosphate scaling while inhibiting metal corrosion, extending equipment lifespan without interfering with system operations—a critical advantage for continuous production environments.

Technical Specifications That Drive Performance

The density (≥1.05 g/cm³ at 20°C) ensures proper dispersion in water systems, while the minimum 6.8% organic phosphonate content guarantees effective chelation of scale-forming ions. The liquid formulation allows for easy dosing and integration into automated chemical feed systems, reducing manual handling errors. pH control (≤4.5 in 1% solution) ensures compatibility with common water treatment chemicals, preventing precipitate formation that could clog filters or reduce heat transfer efficiency.

Quality Assurance for Long-Term Operational Stability

Choosing a high-purity Organic Phosphonate Inhibitor for Industrial Water minimizes the risk of unexpected downtime caused by inhibitor degradation or batch variability. Our product complies with industrial water treatment standards, supporting compliance with ISO 9001 quality management systems. Unlike low-quality alternatives that may contain heavy metal impurities or inconsistent active ingredient levels, our inhibitor provides predictable performance, reducing maintenance costs and ensuring process reliability.

Stringent Quality Control for Confident Application

Every batch undergoes comprehensive testing including density measurement, pH analysis, and organic phosphonate content verification using HPLC. With a production capacity of 15,000 tons/year, we maintain stable supply chains to prevent material shortages. Each delivery includes a batch-specific Certificate of Analysis, and our technical team provides application guidance to optimize dosing rates based on water hardness, flow rate, and system conditions.

Certificate of Analysis & Documentation

All shipments include a detailed Certificate of Analysis (COA) with batch-specific test results and safety data sheet (MSDS). Customers can request additional documentation such as material safety data or technical specifications for regulatory compliance purposes.

Storage & Handling

  • Store in a cool, dry, well-ventilated area, sealed and away from direct sunlight.
  • Keep away from incompatible materials, food and feed sources.
  • Handle with appropriate personal protective equipment (gloves, goggles, lab coat).
  • Follow good industrial hygiene practices. Avoid inhalation and skin contact.
  • Refer to MSDS for detailed storage and safety instructions.

Streamlined Order Process for Industrial and Research Needs

Submit your request with required volume and delivery timeline, and our team will provide a quotation within 24 hours. For first-time users, small-batch samples (25kg drum) are available for compatibility testing. Bulk orders (200kg/1ton drums) ship within 7-15 days via logistics partners specializing in chemical transport, with full tracking provided from dispatch to delivery.

Frequently Asked Questions

Q: What is the shelf life of this inhibitor?

A: The product has a shelf life of 1 year when stored in original sealed containers under recommended conditions.

Q: Can this product be used in potable water systems?

A: No, this inhibitor is for industrial and laboratory research use only, not for applications involving direct human consumption.

Q: What documentation is provided with each order?

A: Each shipment includes a Certificate of Analysis (COA) and Material Safety Data Sheet (MSDS).

Q: Are custom packaging options available?

A: Standard packaging includes 25kg, 200kg, and 1 ton drums; custom packaging may be available for large-volume orders.

Q: How is the organic phosphonate content verified?

A: Organic phosphonate content (as PO43-) is tested using HPLC analysis, with results ≥6.8% guaranteed per batch.
Usage Notice: Supplied exclusively for industrial manufacturing and laboratory research purposes. The buyer is fully responsible for complying with all local laws, regulations and safety requirements for its use.
Industry Solutions

Designed for Modern Chemical Industry

Meeting the demands of dual-carbon goals with green, efficient new material solutions.

⚗️

New Catalysts

High-performance catalysts for energy-efficient chemical processes

🌱

Eco-friendly Materials

Bio-based and biodegradable materials for sustainable manufacturing

🔩

Special Polymers

High-performance polymers for demanding industrial applications

🤝

Custom R&D

Collaborative development from concept to commercial production

Our Cooperation Process

From your initial inquiry to long-term technical partnership -- a transparent, efficient workflow.

📋
01 Submit Requirement
🔍
02 Technical Evaluation
🧪
03 Sample Testing
⚙️
04 Formula Optimization
🏭
05 Trial Production
🚀
06 Mass Delivery & Support

Request a Quote

Tell us your requirements and our technical team will respond within 24 hours.

By submitting, you agree to our privacy policy.

Related Products

Water Treatment Chemicals

Reverse Osmosis Scale Inhibitor RO Antiscalant for Concentrated Water with Acidic Formula 25kg Drum

<p>Keep your reverse osmosis system running at peak efficiency with our <strong>Reverse Osmosis Scale Inhibitor</strong>—an acidic formula designed to prevent mineral buildup in concentrated water streams, ensuring consistent performance and extending equipment lifespan. Perfect for labs and small-scale operations, this 25kg drum delivers the precise quantity you need without excess waste, solving the frustration of oversized minimum orders.</p><ul><li>Acidic formulation (pH 2.0±1.0) effectively inhibits scale formation in high-concentration RO systems</li><li>Colorless to light yellow transparent liquid blends seamlessly into your water treatment process</li><li>Small-batch availability ensures fast 7-15 day delivery to keep your R&D or production on track</li></ul>

View Details
Water Treatment Chemicals

Dpnba Non-Oxidizing RO Membrane Fungicide for Bactericidal Antibacterial Protection 25kg

<p>Keep your RO membrane systems protected with fast-acting bactericidal and antibacterial defense using our <strong>Dpnba RO Membrane Fungicide</strong>. This non-oxidizing biocide delivers reliable microbial control without compromising membrane integrity, ensuring your filtration processes stay efficient even with time-sensitive projects.</p><ul><li>Colorless to light yellow transparent liquid formulation (pH 2.0-7.0) designed for seamless integration into RO system maintenance routines</li><li>25kg plastic bucket packaging meets small-batch needs, so you get exactly what you require without excess inventory</li><li>Factory-direct supply ensures quick turnaround, letting you address urgent microbial growth concerns before they impact performance</li></ul>

View Details
Construction Chemicals

Mineral Oil Defoamer SGR1840W for Construction Industry with Self-Emulsifiable Dispersibility

<p>Speed up construction projects with reliable foam control using our <strong>Mineral Oil Defoamer SGR1840W</strong>—designed to eliminate air bubbles quickly in concrete, coatings, and other building materials without slowing down your workflow. Its self-emulsifiable dispersibility ensures easy mixing into water-based systems, saving time on preparation while maintaining 99% solid content for long-lasting defoaming and suppression.</p><ul><li>Light yellow/amber liquid formula with 50-500 MPa.S viscosity adapts to various construction applications</li><li>Stable emulsion (6 months shelf life) and cool-dry storage requirement ensure product integrity on job sites</li><li>Available in 25kg, 200kg, or 1-ton drums to fit your project scale, delivered fast to keep R&D and production on track</li></ul>

View Details