Frozen Brine Corrosion Inhibitors for Calcium Chloride Sodium Chloride Refrigerant Systems with pH ≥8.0

Frozen Brine Corrosion Inhibitors for Calcium Chloride Sodium Chloride Refrigerant Systems with pH ≥8.0

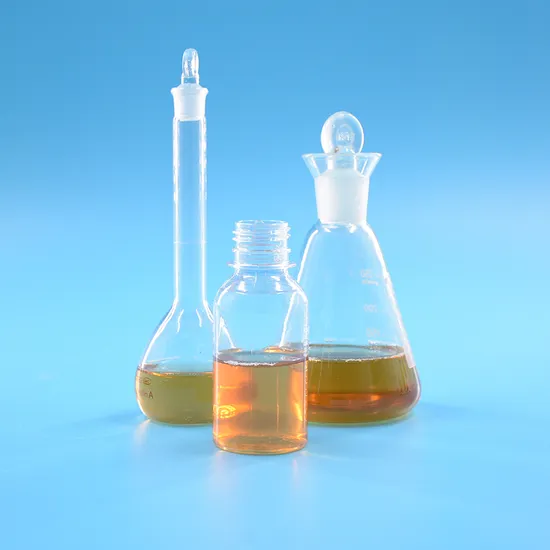
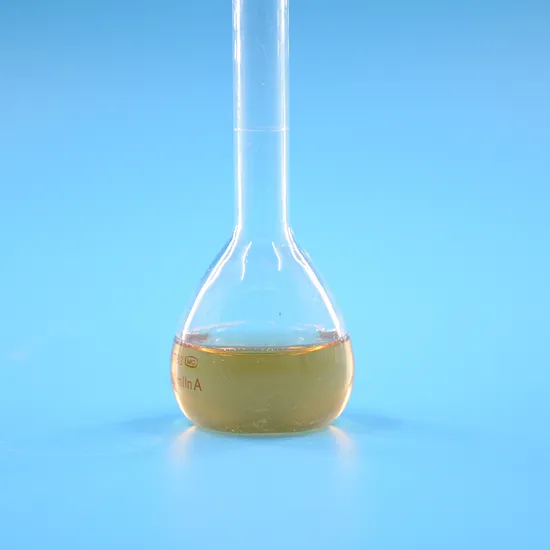
Protect your calcium chloride and sodium chloride refrigerant systems from corrosion with our reliable Frozen Brine Corrosion Inhibitors, ensuring smooth operation even in demanding low-temperature environments. Formulated to maintain a pH ≥8.0, this amber liquid solution (Model SGR-0813W) creates a protective barrier that extends equipment lifespan and reduces maintenance interruptions.

  • Industrial-grade liquid formula with a density of ≥1.1g/cm³ (20°C) for optimal performance in circulating systems
  • Flexible packaging options (25 kg/drum, 1 ton/drum, or custom) to suit small-batch trial needs and urgent orders
  • One-year shelf life ensures long-term storage stability, perfect for laboratories and R&D teams

Backed by factory-direct supply from Shandong, this inhibitor delivers consistent results without the wait—ideal for keeping your refrigeration projects on track.

Quality Certified
Technical Support
Custom R&D

Product Details

FOR INDUSTRIAL AND LABORATORY RESEARCH USE ONLY. NOT FOR DIRECT HUMAN CONSUMPTION, THERAPEUTIC OR HOUSEHOLD USE.
For industrial manufacturing and laboratory research purposes only.

Product Specifications

Parameter Value
Color Amber Colored
Appearance Liquid
Type Industrial Circulating Water Treatment Agent
Shelf Life One Year
pH(1% Aqueous Solution) ≥8.0
Density (20°C) G/Cm³ ≥1.1g/cm3
Transport Package Blue Plastics Drum, White Plastics Drum
Specification 25 kg/drum 1 ton/drum or as your requirement
Trademark GIDINEW
Origin Jining City, Shandong Province, China
HS Code 2917190090

Frozen Brine Corrosion Inhibitors: Solving Refrigerant System Corrosion in Calcium Chloride and Sodium Chloride Solutions

We've witnessed countless R&D projects and small-batch production runs delayed by corrosion issues in calcium chloride and sodium chloride refrigerant systems. Traditional suppliers often force high minimum order quantities for corrosion inhibitors, leaving laboratories and startups with excess inventory or subpar alternatives that fail to meet pH requirements, ultimately compromising system integrity and research timelines.

Stable pH ≥8.0 Formula for Reliable Refrigerant System Protection

Our Frozen Brine Corrosion Inhibitors address these challenges with a specialized formulation designed for calcium chloride and sodium chloride refrigerant systems. As a fast-response chemical service provider, we understand the urgency of R&D and small-batch production needs, offering flexible quantities that eliminate the burden of excessive minimum orders while ensuring consistent performance with a pH level of ≥8.0.

Key Applications in Industrial Refrigeration and Research Settings

This Refrigerant System Inhibitor is ideal for industrial circulating water treatment in low-temperature refrigeration processes, including food processing, pharmaceutical manufacturing, and laboratory cooling systems. Its liquid form allows for easy integration into existing brine solutions, providing effective corrosion protection without disrupting system operations—strictly for industrial and laboratory use only.

Critical Specifications for Optimal Corrosion Inhibition Performance

The pH(1% aqueous solution) of ≥8.0 is paramount for maintaining the chemical stability required to form a protective film on metal surfaces, preventing pitting and rust in chloride-rich environments. With a density of ≥1.1g/cm³ at 20°C, the inhibitor ensures proper dispersion and contact with system components, while its amber liquid appearance allows for visual confirmation of uniform mixing. The one-year shelf life guarantees product efficacy from delivery to application, crucial for research continuity and production planning.

Benefits of Choosing Our Small Batch Frozen Brine Corrosion Inhibitors

Opting for our corrosion inhibitors reduces the risk of equipment failure and costly downtime compared to using untested alternatives. Our factory-direct supply chain ensures quality control at every stage, meeting industry standards for industrial water treatment agents. For research institutions and small-scale producers, our flexible packaging options—from 25 kg drums to 1 ton containers—minimize waste and storage costs, while our 24-hour response time ensures your projects stay on schedule.

Quality Assurance You Can Rely On

Each batch of our Frozen Brine Corrosion Inhibitors undergoes rigorous testing to verify pH, density, and corrosion inhibition efficiency. We provide a Certificate of Analysis (COA) with every order, detailing key parameters for your quality records. With a production capacity of 15000 Ton/Year, we maintain stable supply even for growing demand, and our dedicated customer service team offers technical support to ensure proper application and maximum performance.

Certificate of Analysis & Documentation

Every shipment includes a batch-specific COA and MSDS, providing comprehensive safety and quality data. Detailed test results for pH, density, and appearance are available upon request, and we can arrange additional third-party testing for critical applications to ensure compliance with your specific requirements.

Storage & Handling

  • Store in a cool, dry, well-ventilated area, sealed and away from direct sunlight.
  • Keep away from incompatible materials, food and feed sources.
  • Handle with appropriate personal protective equipment (gloves, goggles, lab coat).
  • Follow good industrial hygiene practices. Avoid inhalation and skin contact.
  • Refer to MSDS for detailed storage and safety instructions.

Simple Ordering Process for Your Refrigerant System Needs

To purchase Frozen Brine Corrosion Inhibitors for your refrigerant system, contact our sales team with your required quantity and packaging preferences. We offer sample testing for qualification, followed by fast production and delivery within 7-15 days for small-batch orders. All shipments include necessary documentation to streamline your receiving and quality control processes.

Frequently Asked Questions

Q: What is the shelf life of this corrosion inhibitor?

A: The shelf life is one year when stored in a cool, dry, and sealed environment away from direct sunlight.

Q: Can this product be used for food or medical applications?

A: No, this product is for industrial and laboratory research use only, not for direct human consumption, therapeutic, or household use.

Q: What documentation is provided with each order?

A: Each order includes a Certificate of Analysis (COA) and Material Safety Data Sheet (MSDS).

Q: Are custom packaging options available?

A: Yes, we offer packaging as per your requirement in addition to standard 25 kg/drum and 1 ton/drum options.

Q: How is the pH level ensured in each batch?

A: Each batch is tested for pH(1% aqueous solution) to confirm it meets the ≥8.0 specification, with results documented in the COA.
Usage Notice: Supplied exclusively for industrial manufacturing and laboratory research purposes. The buyer is fully responsible for complying with all local laws, regulations and safety requirements for its use.
Industry Solutions

Designed for Modern Chemical Industry

Meeting the demands of dual-carbon goals with green, efficient new material solutions.

⚗️

New Catalysts

High-performance catalysts for energy-efficient chemical processes

🌱

Eco-friendly Materials

Bio-based and biodegradable materials for sustainable manufacturing

🔩

Special Polymers

High-performance polymers for demanding industrial applications

🤝

Custom R&D

Collaborative development from concept to commercial production

Our Cooperation Process

From your initial inquiry to long-term technical partnership -- a transparent, efficient workflow.

📋
01 Submit Requirement
🔍
02 Technical Evaluation
🧪
03 Sample Testing
⚙️
04 Formula Optimization
🏭
05 Trial Production
🚀
06 Mass Delivery & Support

Request a Quote

Tell us your requirements and our technical team will respond within 24 hours.

By submitting, you agree to our privacy policy.

Related Products

Petroleum Chemicals

Petroleum Coke Demulsifier SGR 1740W for Quick Dewatering Industrial Processing

<p>Speed up petroleum coke processing with fast, reliable dewatering using <strong>Petroleum Coke Demulsifier SGR 1740W</strong>. This colorless to yellow transparent liquid efficiently solves demulsification and separation challenges, ensuring your industrial processes stay on track without delays. <strong>Do not mix with other demulsifiers</strong> to maintain optimal performance—we’ve seen firsthand how this simple step prevents costly process disruptions.</p> <ul> <li>200kg plastic bucket packaging fits seamlessly into small-batch operations, eliminating the hassle of excess inventory</li> <li>Delivers consistent results in industrial settings, reducing downtime and keeping R&D or production moving forward</li> </ul>

View Details
Water Treatment Chemicals

Reverse Osmosis Scale Inhibitor Phosphorus-Free for Food Beverage Plant Water Purification

<p>Keep your food and beverage plant’s water purification system running at peak efficiency with our <strong>reverse osmosis scale inhibitor phosphorus-free</strong> solution. This advanced membrane chemical prevents scale buildup in RO systems, ensuring consistent water quality and reducing costly downtime from clogged membranes—perfect for meeting tight production schedules without compromising on safety.</p> <ul> <li>Formulated as a colorless or pale yellow transparent liquid with a pH of ≥9.0, it delivers reliable scale inhibition in food-grade applications</li> <li>Factory-direct supply ensures fast delivery of small-batch orders, so you can address urgent maintenance needs without waiting for bulk minimums</li> <li>Protects RO membranes from mineral deposits, extending equipment lifespan and maintaining optimal water flow for your production line</li> </ul>

View Details
Water Treatment Chemicals

pH Stable Quaternary Ammonium Salt Non-Oxidizing Bactericidal Algaecide for Industrial Circulating Water Treatment

<p>Maintain consistent microbial control in industrial circulating water systems with our <strong>pH stable quaternary ammonium salt non-oxidizing bactericidal algaecide</strong>, designed to eliminate biofilm and algae growth without disrupting water chemistry. Its colorless to light yellow liquid formulation (16.0%+ active substance) ensures easy integration into existing treatment processes, while the ≤8.0 pH in 1% solution guarantees stability across typical operating ranges—no need for frequent pH adjustments that slow down your workflow.</p><ul><li>Delivers reliable bactericidal action in industrial circulating water, preventing equipment fouling and maintaining system efficiency</li><li>25kg plastic bucket packaging supports flexible small-batch ordering, so you only stock what you need without excess inventory</li><li>Density of 0.9~1.1 g/cm³ at 20°C ensures compatibility with standard dosing systems for seamless application</li></ul>

View Details