For industrial manufacturing and laboratory research purposes only.
Product Specifications
| Parameter | Value |
|---|---|
| Model NO. | ProtectMBC 1571W |
| Color | Colorless or White Liquid |
| Appearance | Liquid |
| Type | Chemicals for Membrane |
| Product Name | Reverse Osmosis Reducer (Liquid) |
| Density | 1.15±0.05 |
| pH | 4.0-6.0 |
| Effect | Eliminate The Risk of Oxidation |
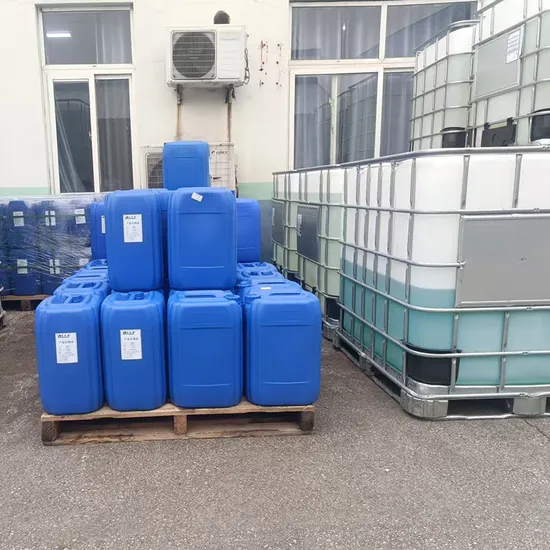
| Transport Package | Plastic Bucket |
| Specification | 25kg |
| Trademark | SCIEN GREEN |
| Origin | Jining City, Shandong Province |
Reverse Osmosis Reducing Agent for Oxidation Protection: Solving Membrane Degradation Challenges
For over a decade in the membrane chemicals industry, we've witnessed countless R&D projects and small-batch production runs derailed by unexpected oxidation damage to reverse osmosis membranes. Traditional suppliers often force minimum order quantities that leave laboratories and startups with excess inventory, while slow delivery times turn urgent protection needs into costly downtime. The struggle to find reliable small-batch Reverse Osmosis Reducing Agent solutions is a recurring pain point for researchers and production managers alike.
A Fast-Response Solution for Membrane Oxidation Risk Elimination
Our Reverse Osmosis Reducing Agent Liquid (ProtectMBC 1571W) is specifically formulated to address these challenges. As a specialized chemical service provider with a 10+ year track record serving 50+ countries, we understand the critical need for both technical precision and operational agility. Our flexible production system enables us to deliver small-batch orders of this RO Reducer Liquid within 7-15 days, with initial quotations and delivery confirmations provided within 24 hours—perfect for university laboratories, startup tech companies, and any operation requiring rapid response to oxidation threats.
Industrial Applications of Membrane Oxidation Risk Elimination Agent
This Colorless Liquid Reducer finds essential application in industrial water treatment systems, research laboratories conducting membrane performance studies, and pilot-scale production facilities where maintaining reverse osmosis membrane integrity is critical. Its primary function as a Membrane Oxidation Risk Elimination Agent makes it invaluable in processes where residual oxidants could compromise membrane structure, including pre-treatment stages in pharmaceutical manufacturing, semiconductor wafer production, and advanced material synthesis research. All applications are strictly limited to industrial and laboratory environments.
Key Specifications Ensuring Optimal Performance
The precise density of 1.15±0.05 g/cm³ ensures consistent dosing accuracy, eliminating the variability that can lead to either under-protection (leaving oxidation risks) or over-treatment (wasting expensive chemicals). The pH range of 4.0-6.0 is specifically calibrated to maintain compatibility with common reverse osmosis membrane materials, preventing pH-induced degradation while maximizing reduction efficiency. As a liquid formulation, it offers superior mixing characteristics compared to powder alternatives, ensuring uniform distribution in treatment systems. The 25kg plastic bucket packaging strikes the ideal balance between laboratory-scale usability and industrial handling efficiency, reducing waste from unused product.
Benefits of Reliable Oxidation Protection for Membrane Systems
Using a validated Reverse Osmosis Reducing Agent like ProtectMBC 1571W translates directly to measurable operational benefits. Laboratories gain confidence in experimental reproducibility by eliminating membrane oxidation variables, while industrial users reduce maintenance costs associated with premature membrane replacement. Our commitment to batch-to-batch consistency, backed by rigorous quality control protocols, ensures that your oxidation protection strategy remains effective over time—avoiding the hidden costs of inconsistent performance from lower-quality alternatives. All production processes adhere to ISO 9001 standards, ensuring compliance with global industrial chemical requirements.
Quality Assurance You Can Verify
Every batch of our Reverse Osmosis Reducing Agent undergoes comprehensive testing, including density measurement, pH analysis, and oxidation reduction potential verification, with results documented in a Certificate of Analysis (COA) provided with each order. Our quality control laboratory is equipped with advanced analytical instruments to ensure specifications are met before any product leaves our facility. We stand behind our product with a straightforward guarantee: if your received material fails to meet the specifications outlined in your COA, we will replace it at no cost. Our technical support team is available to assist with application questions, drawing on years of experience in membrane chemical formulation and use.
Certificate of Analysis & Documentation
Each shipment includes a batch-specific Certificate of Analysis detailing all tested parameters, along with a Material Safety Data Sheet (MSDS) containing handling, storage, and emergency procedures. For research institutions requiring detailed analytical data, additional test results can be provided upon request, including chromatographic profiles and stability studies relevant to long-term storage.
Storage & Handling
- Store in a cool, dry, well-ventilated area, sealed and away from direct sunlight.
- Keep away from incompatible materials, food and feed sources.
- Handle with appropriate personal protective equipment (gloves, goggles, lab coat).
- Follow good industrial hygiene practices. Avoid inhalation and skin contact.
- Refer to MSDS for detailed storage and safety instructions.
Simple Order Process for Your Oxidation Protection Needs
Initiate your order by sending your specific requirements—including quantity and delivery timeline—to our technical sales team. We provide detailed product specifications and can arrange sample testing for qualification in your specific application. Once specifications are confirmed, orders are processed immediately to meet our 7-15 day delivery commitment. All shipments include the documentation needed for regulatory compliance and quality assurance, ensuring a seamless procurement experience for both research and production applications.
Frequently Asked Questions
Q: What is the shelf life of ProtectMBC 1571W when properly stored?
A: When stored in unopened original packaging under recommended conditions, the product maintains stability for 12 months from the date of manufacture, as indicated on the container label.
Q: Is this product suitable for use in food or pharmaceutical production applications?
A: This product is intended FOR INDUSTRIAL AND LABORATORY RESEARCH USE ONLY. It is not certified for direct contact with food, pharmaceuticals, or medical devices.
Q: What documentation is provided with each order?
A: Every shipment includes a Certificate of Analysis (COA) specific to the batch and a Material Safety Data Sheet (MSDS) with handling and safety information.
Q: Can the packaging size be customized for specific laboratory needs?
A: While our standard packaging is 25kg plastic buckets, we offer smaller container options for laboratory-scale requirements. Contact our sales team to discuss custom packaging solutions.
Q: How is the effectiveness of the oxidation reduction capability verified?
A: Each batch undergoes redox potential testing to confirm reduction capacity, with results documented in the COA. Additional performance testing can be arranged for specific applications.