
For industrial manufacturing and laboratory research purposes only.
Product Specifications
| Parameter | Value |
|---|---|
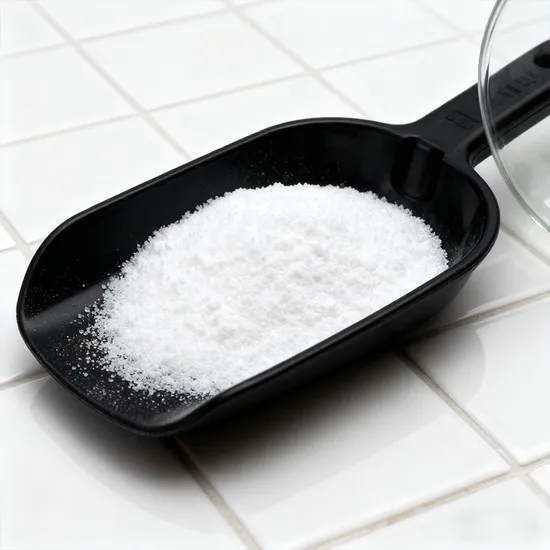
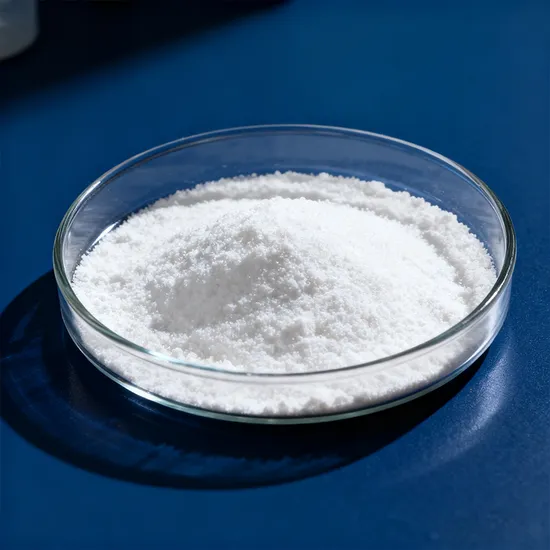
| Color | White Granular Solid |
| Appearance | Granulars |
| Type | Chemicals for Membrane |
| Product Name | Reverse Osmosis Flocculant (Organic) |
| Solid Content | ≥85% |
| Effect | Effectively Coagulate Suspended Organic Colloids |
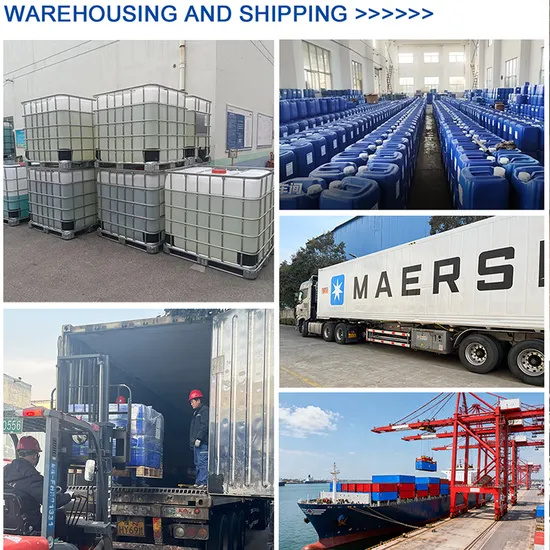
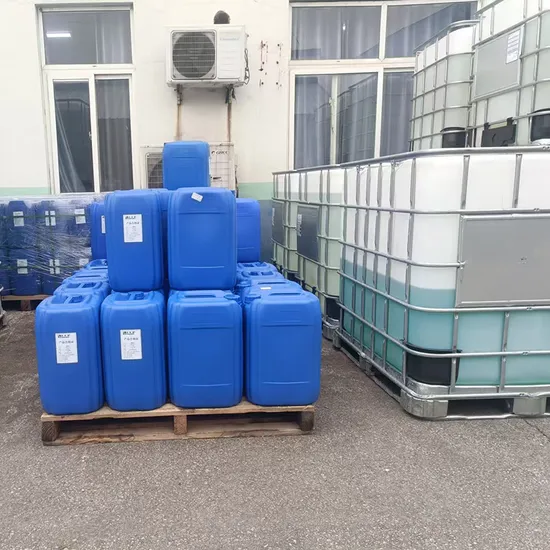
| Transport Package | Plastic Round Bucket/Bagged |
| Specification | 25kg |
| Trademark | GIDINEW |
| Origin | Jining City, Shandong Province |
Organic Reverse Osmosis Flocculant ProtectMBC 1580W: Addressing Water Treatment Challenges in Power and Steel Plants
In water treatment operations for power plants and steel plants, we've witnessed how traditional flocculants often fail to meet the demands of reverse osmosis systems—either leaving residual colloids that foul membranes or requiring excessive dosage that increases operational costs. Research teams and plant managers consistently report delays in R&D trials or production shutdowns due to suppliers unable to deliver small-batch, high-quality flocculants with reliable performance.
A Tailored Solution for Membrane Protection and Efficient Coagulation
Our Reverse Osmosis Flocculant Organic ProtectMBC 1580W is engineered to resolve these critical pain points. With a flexible production system capable of delivering small-batch orders within 7-15 days, we ensure that your R&D timelines and emergency production needs are met without compromise. The product’s granular form and high solid content (≥85%) guarantee consistent mixing and dosage accuracy, addressing the common issue of batch-to-batch variability that plagues laboratory research and industrial trials.
Industrial Applications in Power and Steel Plant Water Treatment
As a specialized Membrane Chemicals, ProtectMBC 1580W is designed for integration into reverse osmosis systems in power plants and steel plants, where efficient removal of suspended organic colloids is essential for maintaining membrane integrity and water purification efficiency. Its application supports pre-treatment processes, preventing membrane fouling and extending the service life of critical water treatment equipment—ultimately reducing maintenance costs and downtime in industrial operations.
The Importance of Key Specifications in Flocculant Performance
The granular appearance of ProtectMBC 1580W ensures easy handling and dissolution, a critical factor in industrial settings where quick deployment is often necessary. Its white color indicates high purity, minimizing the risk of introducing unwanted contaminants into water treatment systems. The solid content of ≥85% translates to higher active ingredient concentration, allowing for lower dosage requirements compared to diluted alternatives—directly reducing material costs and waste. Most importantly, its proven effect in coagulating suspended organic colloids ensures that reverse osmosis membranes operate at peak efficiency, a specification validated through rigorous performance testing.
Benefits of Choosing a Reliable Organic Flocculant Supplier
Opting for a high-quality Organic Flocculant like ProtectMBC 1580W mitigates the risks associated with substandard products, such as membrane damage, inconsistent water quality, and regulatory non-compliance. Our commitment to ISO 9001 standards ensures that every batch meets strict quality criteria, while our ability to provide small-batch orders eliminates the burden of excessive minimum order quantities that often plague traditional suppliers. This balance of quality and flexibility delivers long-term value by aligning with both R&D scalability and industrial production efficiency.
Our Commitment to Quality and Transparency
We maintain rigorous quality control through multiple stages of testing, including composition analysis and performance validation, to ensure each batch of ProtectMBC 1580W meets advertised specifications. Every order is accompanied by a Certificate of Analysis (COA) detailing key parameters, providing full traceability for your records. Our 10+ years of experience in serving industrial and laboratory clients worldwide, combined with a dedicated customer service team available 24/7, ensures that technical support and order updates are always accessible. If a product fails to meet your specified requirements, we offer a straightforward return and replacement process, underscoring our confidence in product consistency.
Certificate of Analysis & Documentation
Each shipment of ProtectMBC 1580W includes a batch-specific COA and Material Safety Data Sheet (MSDS), providing comprehensive information on product specifications, handling precautions, and safety guidelines. For research or regulatory purposes, detailed testing data can be requested using your order number, ensuring full compliance with documentation requirements for industrial and laboratory use.
Storage & Handling
- Store in a cool, dry, well-ventilated area, sealed and away from direct sunlight.
- Keep away from incompatible materials, food and feed sources.
- Handle with appropriate personal protective equipment (gloves, goggles, lab coat).
- Follow good industrial hygiene practices. Avoid inhalation and skin contact.
- Refer to MSDS for detailed storage and safety instructions.
Streamlined Order Process for Your Convenience
To place an order for ProtectMBC 1580W, simply submit your requirements via email or phone, and our team will provide a detailed quotation within 24 hours. For first-time users, we offer sample quantities to facilitate compatibility testing in your specific water treatment system. Once specifications are confirmed, bulk orders are processed and delivered via expedited logistics to ensure timely arrival, with full tracking available throughout the shipping process.
Frequently Asked Questions
Q: What is the shelf life of ProtectMBC 1580W?
A: When stored in sealed packaging under recommended conditions, the product maintains stability for 12 months from the date of manufacture.
Q: Can this flocculant be used in food or pharmaceutical applications?
A: No. ProtectMBC 1580W is intended exclusively for industrial and laboratory research use and must not be used in applications involving direct human consumption.
Q: What documentation is provided with each order?
A: Each shipment includes a Certificate of Analysis (COA) and Material Safety Data Sheet (MSDS) specific to the batch.
Q: Do you offer customized packaging or specifications?
A: Yes, we support small-batch customized synthesis and can accommodate specific packaging requirements for industrial clients.
Q: How is the product's effectiveness in coagulating colloids verified?
A: Each batch undergoes performance testing to confirm its ability to coagulate suspended organic colloids, with results documented in the COA.