Boiler Reclaimed Water Corrosion Inhibitor SGR-1906W Removes Residual Rust Enhances Exchange Efficiency

Boiler Reclaimed Water Corrosion Inhibitor SGR-1906W Removes Residual Rust Enhances Exchange Efficiency

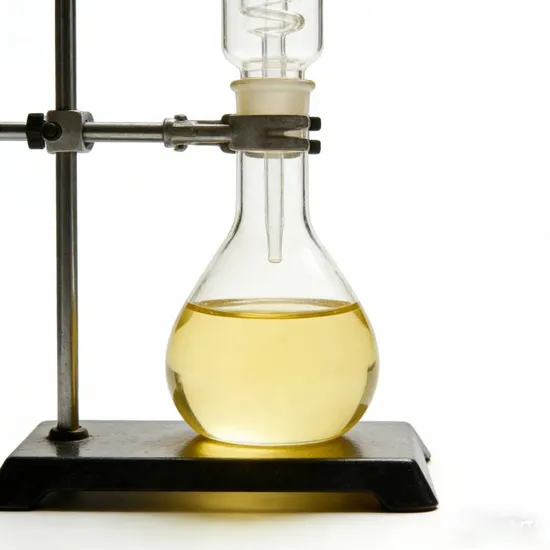
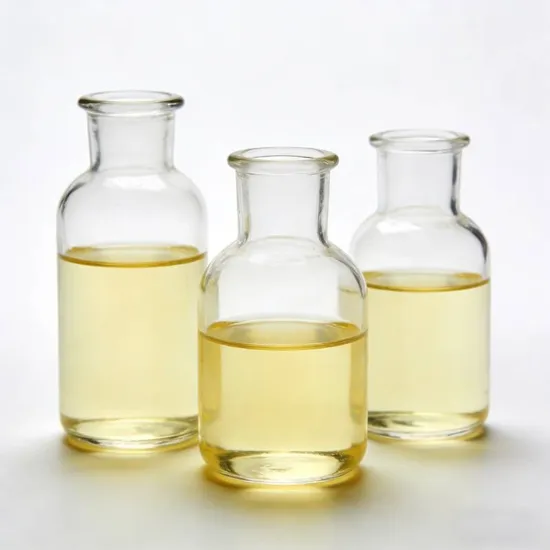
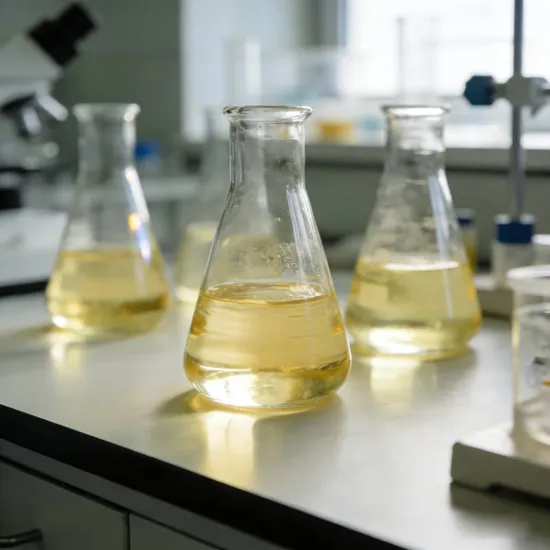
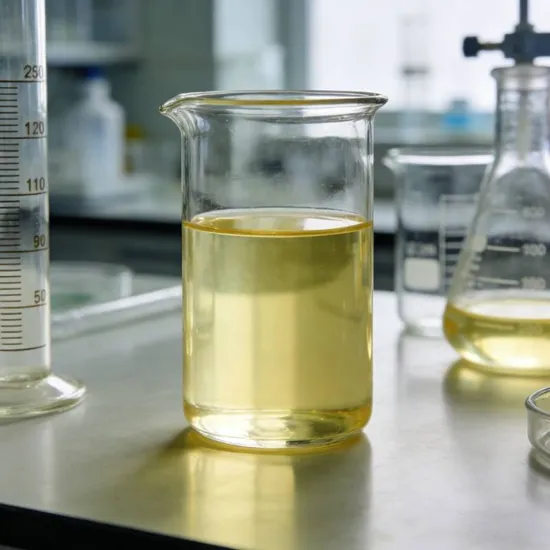
Eliminate residual rust and boost heat exchange efficiency in your boiler system with Boiler Reclaimed Water Corrosion Inhibitor SGR-1906W, a specialized water treatment chemical designed for reclaimed water applications. Its high alkalinity (pH ≥12) forms a protective barrier against corrosion, while the light yellow liquid formula ensures easy integration into existing water treatment processes—perfect for facilities needing reliable performance without disrupting operations.

  • Accelerates R&D and trial production timelines with fast 7-15 day delivery on small-batch orders
  • Maintains system integrity with a base value of 555.0-613 mgKOH/g, meeting strict industrial standards
  • Flexible packaging options (25 kg/drum, 1 ton/drum, or custom) adapt to your specific operational needs
Quality Certified
Technical Support
Custom R&D

Product Details

FOR INDUSTRIAL AND LABORATORY RESEARCH USE ONLY. NOT FOR DIRECT HUMAN CONSUMPTION, THERAPEUTIC OR HOUSEHOLD USE.
For industrial manufacturing and laboratory research purposes only.

Product Specifications

Parameter Value
Color Light Yellow
Appearance Liquid
Type Chemicals for Boilers
Shelf Life One Year
pH ≥12
Density (20°C), G/Cm³ <1.0
Base Value of Mgkoh / G 555.0-613
Transport Package Blue Plastics Drum, White Plastics Drum
Specification 25 kg/drum 1 ton/drum or as your requirement
Trademark GIDINEW
Origin Jining City, Shandong Province, China
Production Capacity 5000ton/Year
Package Size 120.00cm * 100.00cm * 115.00cm
Package Gross Weight 1054.000kg

Overcoming Boiler Reclaimed Water Corrosion Challenges with SGR-1906W Inhibitor

For over a decade in the water treatment chemical industry, we've witnessed how residual rust accumulation and inefficient heat exchange in boiler systems can cripple industrial operations and delay critical research projects. Traditional inhibitors often fail to address both issues simultaneously, forcing facilities to compromise on either corrosion protection or system performance—a problem we've solved through years of formulation refinement.

Boiler Reclaimed Water Corrosion Inhibitor: The Dual-Action Solution

Our SGR-1906W Boiler Reclaimed Water Corrosion Inhibitor is engineered to tackle the core challenges of reclaimed water systems. As a fast-response chemical service provider, we understand the urgency of R&D and small-batch production needs, which is why this inhibitor delivers both residual rust removal and enhanced heat exchange efficiency in a single application—eliminating the need for multiple chemical treatments.

Industrial Applications of SGR-1906W Inhibitor

This reclaimed water inhibitor finds critical use in industrial boiler systems, power generation facilities, and research laboratories where water recycling is essential. Its liquid formulation ensures easy integration into existing water treatment processes, making it ideal for both continuous operation and pilot-scale testing. By focusing on industrial and laboratory applications, we ensure compliance with strict operational standards without compromising on performance.

Key Specifications Driving Performance

The technical parameters of SGR-1906W directly impact its effectiveness in real-world conditions. With a pH of ≥12, it creates an alkaline environment that passivates metal surfaces, preventing new corrosion while the base value of 555.0-613 mgKOH/g indicates strong rust-dissolving capacity. The density <1.0 g/cm³ ensures uniform dispersion in water systems, while the liquid appearance allows for precise dosing—critical factors in maintaining consistent heat exchange efficiency and corrosion protection across varying system sizes.

Benefits of Using SGR-1906W Boiler Inhibitor

Choosing a high-quality boiler corrosion inhibitor like SGR-1906W minimizes the risk of equipment downtime and maintenance costs associated with substandard products. Unlike generic inhibitors, our formulation meets industrial-grade standards, ensuring compatibility with reclaimed water's unique chemistry. With a one-year shelf life and flexible packaging options, it provides long-term supply stability—reducing the logistical challenges of frequent reordering and storage management for both large-scale operations and research facilities.

Quality Assurance You Can Verify

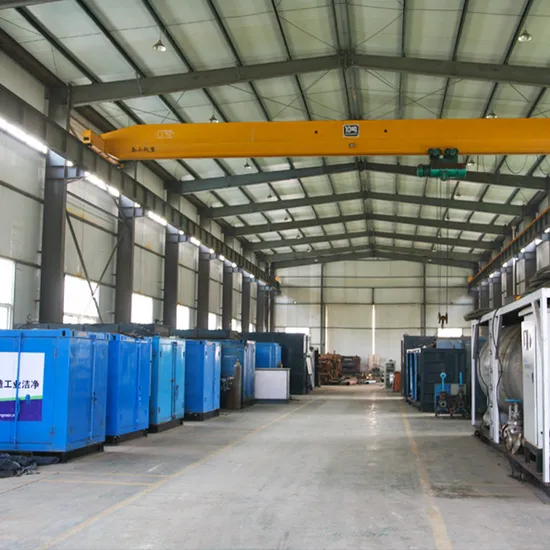
Our commitment to quality is backed by rigorous testing protocols. Each batch of SGR-1906W undergoes comprehensive analysis, including pH verification, density measurement, and base value testing, to ensure compliance with specifications. As a factory-direct supplier with a 5000-ton annual production capacity, we maintain full control over the manufacturing process, from raw material selection to final packaging. This vertically integrated approach allows us to provide consistent quality and traceability for every order.

Certificate of Analysis & Documentation

Every shipment of SGR-1906W includes a detailed Certificate of Analysis (COA) with batch-specific test results, ensuring complete transparency of product quality. Material Safety Data Sheets (MSDS) are also provided to support safe handling and regulatory compliance. For research institutions requiring additional documentation, specific test records can be requested using your order reference number.

Storage & Handling

  • Store in a cool, dry, well-ventilated area, sealed and away from direct sunlight.
  • Keep away from incompatible materials, food and feed sources.
  • Handle with appropriate personal protective equipment (gloves, goggles, lab coat).
  • Follow good industrial hygiene practices. Avoid inhalation and skin contact.
  • Refer to MSDS for detailed storage and safety instructions.

Streamlined Ordering Process

To ensure your project stays on schedule, we offer a straightforward procurement process: submit your requirements via email or phone, receive a customized quotation within 24 hours, confirm your order details, and receive your shipment in 7-15 days. We accommodate both standard 25 kg/drum packaging and custom sizes to meet your specific operational needs, with full logistics tracking provided from dispatch to delivery.

Frequently Asked Questions

Q: What is the shelf life of SGR-1906W Boiler Reclaimed Water Corrosion Inhibitor?

A: The product has a shelf life of one year when stored in a cool, dry, well-ventilated area and kept sealed away from direct sunlight.

Q: Can this inhibitor be used for food or pharmaceutical applications?

A: No, SGR-1906W is intended FOR INDUSTRIAL AND LABORATORY RESEARCH USE ONLY. It is not suitable for direct human consumption, therapeutic, or household use.

Q: What documentation is provided with each order?

A: Every shipment includes a Certificate of Analysis (COA) with batch-specific test results and a Material Safety Data Sheet (MSDS).

Q: Does the supplier offer custom packaging options?

A: Yes, standard packaging is 25 kg/drum or 1 ton/drum, and custom specifications are available upon request.

Q: How is the product's effectiveness guaranteed?

A: Each batch undergoes rigorous testing for pH, density, base value, and appearance, with results provided in the COA. The manufacturing process adheres to industrial quality standards.
Usage Notice: Supplied exclusively for industrial manufacturing and laboratory research purposes. The buyer is fully responsible for complying with all local laws, regulations and safety requirements for its use.
Industry Solutions

Designed for Modern Chemical Industry

Meeting the demands of dual-carbon goals with green, efficient new material solutions.

⚗️

New Catalysts

High-performance catalysts for energy-efficient chemical processes

🌱

Eco-friendly Materials

Bio-based and biodegradable materials for sustainable manufacturing

🔩

Special Polymers

High-performance polymers for demanding industrial applications

🤝

Custom R&D

Collaborative development from concept to commercial production

Our Cooperation Process

From your initial inquiry to long-term technical partnership -- a transparent, efficient workflow.

📋
01 Submit Requirement
🔍
02 Technical Evaluation
🧪
03 Sample Testing
⚙️
04 Formula Optimization
🏭
05 Trial Production
🚀
06 Mass Delivery & Support

Request a Quote

Tell us your requirements and our technical team will respond within 24 hours.

By submitting, you agree to our privacy policy.

Related Products

Water Treatment Chemicals

Circulating Water Product Heating System Scale and Corrosion Inhibitor for Industrial Circulating Water Treatment

<p>Keep your industrial heating systems running efficiently with our <strong>Circulating Water Product Heating System Scale and Corrosion Inhibitor</strong>—a specialized circulating water treatment agent that prevents scale buildup and corrosion to minimize downtime and extend equipment life. Ideal for R&D trials and small-batch production, this pale yellow to brownish-yellow liquid delivers reliable performance without the hassle of large minimum orders.</p><ul><li>Formulated with ≥6.8% organophosphonates for robust inhibition in high-temperature environments</li><li>Balanced pH (≥1.05 in 1% solution) ensures compatibility with common heating system materials</li><li>Flexible 25kg plastic bucket packaging fits perfectly into small-scale testing and pilot projects</li></ul><p>Backed by DidiChem’s 7-15 day fast delivery, this inhibitor lets you stay on schedule with your industrial water treatment R&D—no more waiting for bulk quantities or compromising on quality for urgent needs.</p>

View Details
Water Treatment Chemicals

Reverse Osmosis Scale Inhibitor Phosphorus-Free for Food Beverage Plant Water Purification

<p>Keep your food and beverage plant’s water purification system running at peak efficiency with our <strong>reverse osmosis scale inhibitor phosphorus-free</strong> solution. This advanced membrane chemical prevents scale buildup in RO systems, ensuring consistent water quality and reducing costly downtime from clogged membranes—perfect for meeting tight production schedules without compromising on safety.</p> <ul> <li>Formulated as a colorless or pale yellow transparent liquid with a pH of ≥9.0, it delivers reliable scale inhibition in food-grade applications</li> <li>Factory-direct supply ensures fast delivery of small-batch orders, so you can address urgent maintenance needs without waiting for bulk minimums</li> <li>Protects RO membranes from mineral deposits, extending equipment lifespan and maintaining optimal water flow for your production line</li> </ul>

View Details
Water Treatment Chemicals

Reverse Osmosis Scale Inhibitors for Reclaimed Water Systems - Effective Inorganic Scaling Control SGR-1505W

<p>Keep your reclaimed water RO systems running at peak efficiency with our <strong>Reverse Osmosis Scale Inhibitors</strong>—SGR-1505W delivers powerful inorganic scaling control to prevent mineral buildup that slows performance and shortens equipment life. As a fast-response chemical provider, we understand the urgency of R&D and small-batch needs, so you can count on tailored quantities (from 25kg drums to 1-ton containers) and reliable delivery that keeps your projects on track.</p><ul><li>Light yellow liquid formula with pH 2.0 ± 1.0 and specific gravity ≥1.05, optimized for RO/NF/UF systems in reclaimed water applications</li><li>Factory-direct supply ensures consistent quality and cost-effectiveness for both trial runs and ongoing operations</li><li>One-year shelf life and flexible packaging options make inventory management simple, even for low-volume requirements</li></ul>

View Details