
For industrial manufacturing and laboratory research purposes only.
Product Specifications
| Parameter | Value |
|---|---|
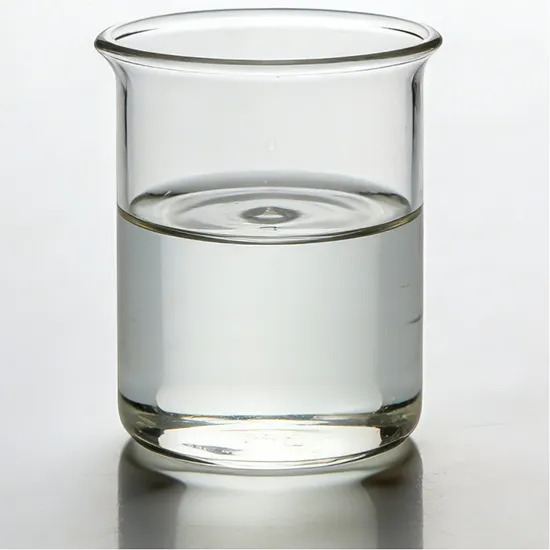
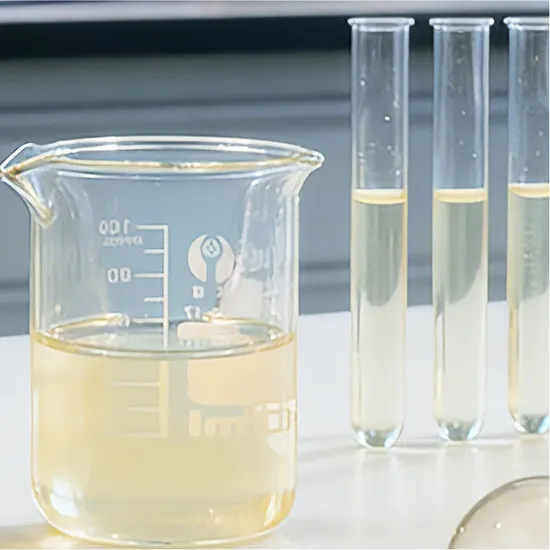
| Color | Colorless or Pale Yellow Transparent Liquid |
| Appearance | Liquid |
| Type | Chemicals for Membrane |
| Product Name | Reverse Osmosis Scale Inhibitor Phosphorus-Free |
| pH(1%) | ≥9.0 |
| Specific Gravity | ≥1.05 |
| Effect | Scale Inhibition and Scale Prevention |
| Transport Package | Plastic Bucket |
| Specification | 25kg |
| Trademark | GIDINEW |
| Origin | Jining City, Shandong Province |
Phosphorus-Free Reverse Osmosis Scale Inhibitor for Food Beverage Plant Water Purification
In food and beverage processing, water purification systems often face critical challenges: traditional scale inhibitors leave phosphorus residues that risk regulatory non-compliance, while substandard inhibitors cause membrane fouling that reduces efficiency by up to 30% within months. Our 10+ years serving beverage plants across 50+ countries have shown these issues directly impact production continuity and product quality.
Advanced Membrane Protection for Food-Grade Water Systems
Our reverse osmosis scale inhibitor phosphorus-free formula addresses these pain points by providing superior scale inhibition without phosphorus compounds, ensuring compliance with food industry standards. With a flexible production system capable of delivering small-batch orders within 7-15 days, we meet the urgent R&D and trial production needs of beverage plant operators and research institutions.
Industrial Applications in Water Purification
This membrane scale prevention chemical is specifically designed for reverse osmosis systems in food and beverage plant water purification. It effectively controls scaling in membrane processes, maintaining optimal water flow and system efficiency. The product is suitable for industrial water treatment applications where phosphorus-free operation is required to meet environmental and quality regulations.
Key Properties and Their Industrial Significance
The alkaline pH (≥9.0) ensures compatibility with typical reverse osmosis system conditions, preventing acid-induced membrane degradation. With a specific gravity of ≥1.05, the liquid formula allows for precise dosing and uniform mixing in water treatment systems. The colorless to pale yellow transparent appearance provides visual confirmation of product purity, while the 25kg plastic bucket packaging ensures safe storage and handling in industrial environments. These specifications work together to deliver consistent scale prevention performance.
Benefits of Phosphorus-Free Scale Inhibition
Using our food grade reverse osmosis inhibitor eliminates the risk of phosphorus discharge violations, which can result in fines and production shutdowns. Unlike conventional phosphorus-based inhibitors, our formula reduces environmental impact while maintaining excellent scale prevention efficacy. The product's reliability translates to lower maintenance costs and extended membrane lifespan, providing long-term value for food and beverage manufacturers. Our compliance with industrial standards ensures seamless integration into existing water purification processes.
Quality Assurance You Can Rely On
Every batch of our reverse osmosis scale inhibitor undergoes rigorous quality control testing, including pH and specific gravity verification, to ensure consistent performance. As a factory direct supplier with 10+ years of experience, we provide full traceability for each production lot. Our professional customer service team responds to technical inquiries within 24 hours, offering expert support for system integration and dosage optimization. We stand behind our product quality with a comprehensive after-sales service guarantee.
Certificate of Analysis & Documentation
Each shipment includes a Certificate of Analysis (COA) with batch-specific test results, ensuring transparency and quality verification. Material Safety Data Sheets (MSDS) are provided for safe handling and regulatory compliance. Detailed technical documentation is available upon request, supporting proper integration into your water purification system.
Storage & Handling
- Store in a cool, dry, well-ventilated area, sealed and away from direct sunlight.
- Keep away from incompatible materials, food and feed sources.
- Handle with appropriate personal protective equipment (gloves, goggles, lab coat).
- Follow good industrial hygiene practices. Avoid inhalation and skin contact.
- Refer to MSDS for detailed storage and safety instructions.
Ordering Process
To place an order, simply send your requirements via email or phone, and our team will provide a fast quotation within 24 hours. We offer sample services for performance evaluation prior to full-scale procurement. Once specifications are confirmed and payment is processed, we begin production and deliver within 7-15 days using the fastest logistics method, with full tracking provided.
Frequently Asked Questions
Q: What is the shelf life of this product?
A: The shelf life is 12 months when stored in original sealed packaging under recommended conditions.
Q: Can this inhibitor be used directly in food or beverage products?
A: No, this product is for industrial water purification system use only, not for direct addition to food or beverage products.
What documentation is provided with each order?
A: Each order includes a Certificate of Analysis (COA) and Material Safety Data Sheet (MSDS).
Q: Is custom packaging available?
A: Standard packaging is 25kg plastic buckets. For special packaging requirements, please contact our sales team to discuss feasibility.
Q: How is the product's scale inhibition performance verified?
A: Each batch undergoes testing to ensure pH and specific gravity meet specifications, which correlate with scale inhibition effectiveness. Full performance data is available in the technical documentation.