

For industrial manufacturing and laboratory research purposes only.
Product Specifications
| Parameter | Value |
|---|---|
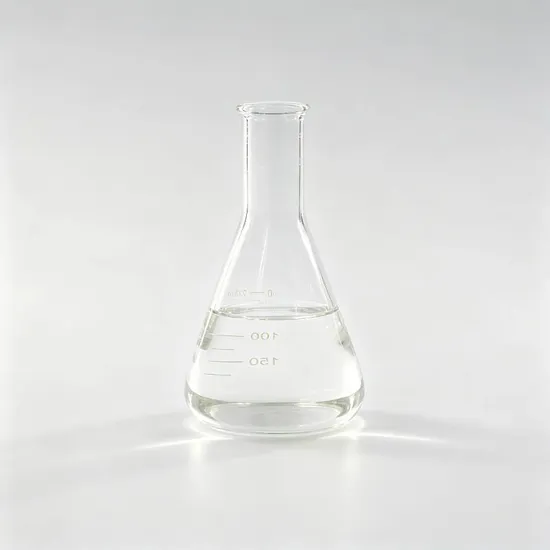
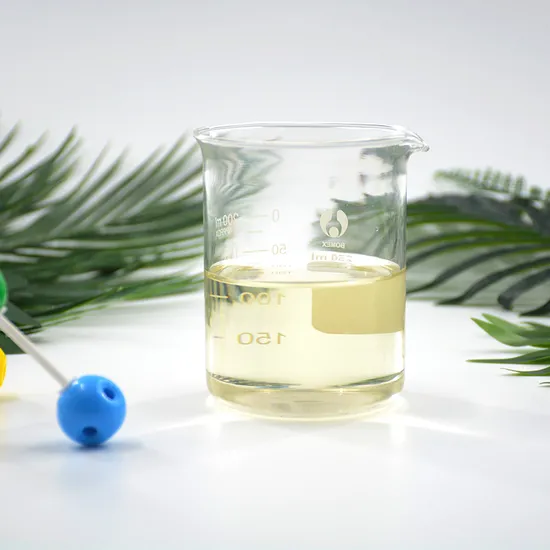
| Color | Colorless to Light Yellow Transparent Liquid |
| Appearance | Liquid |
| Type | Chemicals for Membrane |
| Product Name | Dpnba Non-Oxidizing Biocide |
| pH | 2.0-7.0 |
| Density | ≥1.05 |
| Supplier | Factory Direct Supply |
| Acidity or Alkalinity | Acidic |
| Effect | Bactericidal and Antibacterial |
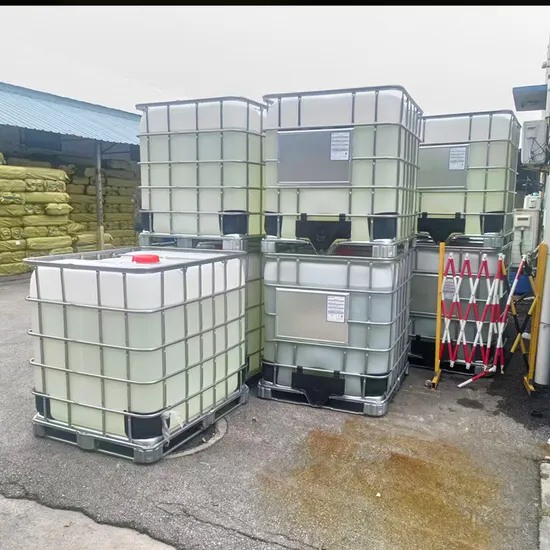
| Transport Package | Plastic Bucket |
| Specification | 25kg |
| Trademark | GIDINEW |
| Origin | Jining City, Shandong Province |
Overcoming Membrane Fouling Challenges with Dpnba Non-Oxidizing Reverse Osmosis Biocide
In industrial membrane systems, persistent bacterial growth often leads to reduced flux rates, increased energy consumption, and frequent maintenance shutdowns. Research laboratories and manufacturing facilities alike struggle with biocides that either corrode membrane materials or require extended contact times, disrupting critical workflow timelines. Having supported over 10,000 industrial clients across 50+ countries, we’ve witnessed how inconsistent biocide performance can derail R&D projects and production schedules.
A Targeted Solution for Membrane System Maintenance
Dpnba Non-Oxidizing Reverse Osmosis Biocide addresses these challenges with its balanced formulation designed for industrial membrane systems. As a fast-response chemical service provider, we ensure that even small-batch orders (starting at 25kg) are delivered within 7-15 days, eliminating the frustration of long lead times that plague traditional bulk suppliers. This biocide’s non-oxidizing nature minimizes membrane degradation risks while providing reliable bactericidal action, making it ideal for both routine maintenance and emergency fouling control.
Key Applications in Industrial Membrane Systems
This Membrane Biocide finds critical use in reverse osmosis (RO) systems, nanofiltration units, and ultrafiltration processes across pharmaceutical manufacturing, semiconductor production, and wastewater treatment facilities. Its bactericidal effect targets biofilm-forming microorganisms without compromising membrane integrity, ensuring consistent performance in high-purity water systems where contamination control is mission-critical.
Why Technical Specifications Drive Performance
The pH range of 2.0-7.0 ensures compatibility with most membrane materials, preventing acid-induced damage that can occur with harsher biocides. A density of ≥1.05 guarantees proper dispersion in water systems, while the colorless to light yellow transparent liquid form allows for easy visual monitoring of dosage levels. The acidic nature enhances bactericidal efficacy by disrupting microbial cell membranes, yet remains mild enough for prolonged use in sensitive industrial processes.
Benefits of Reliable Biocide Supply
Using a standardized Dpnba Non-Oxidizing Biocide reduces the risk of production downtime caused by unexpected fouling events. Unlike generic biocides that may vary batch-to-batch, our strict quality control processes ensure consistent performance, supported by ISO 9001 certification. This reliability translates to lower long-term costs by extending membrane lifespan and reducing maintenance frequency—critical factors for both research labs optimizing experimental conditions and manufacturers scaling production.
Our Commitment to Quality Assurance
Every batch of Dpnba Membrane Biocide undergoes rigorous testing, including density verification and pH analysis, with full documentation available upon request. We provide a Certificate of Analysis (COA) with each shipment, detailing key parameters to ensure compliance with your specific application requirements. Our production facility maintains ISO 9001 standards, and we offer technical support to help optimize dosage and application protocols for your unique membrane system.
Certificate of Analysis & Documentation
Each 25kg plastic bucket is accompanied by a batch-specific COA and MSDS, providing detailed safety and handling information. For research institutions requiring additional verification, specific test data and stability studies can be provided to support experimental reproducibility.
Storage & Handling
- Store in a cool, dry, well-ventilated area, sealed and away from direct sunlight.
- Keep away from incompatible materials, food and feed sources.
- Handle with appropriate personal protective equipment (gloves, goggles, lab coat).
- Follow good industrial hygiene practices. Avoid inhalation and skin contact.
- Refer to MSDS for detailed storage and safety instructions.
Streamlined Order Process for Your Convenience
Initiate your order by contacting our technical team with your specific membrane system requirements. We provide fast quotations within 24 hours, including sample availability for pre-testing in your facility. Once specifications are confirmed, production begins immediately to ensure delivery within our 7-15 day window, with full logistics tracking provided until arrival.
Frequently Asked Questions
Q: What is the recommended shelf life of Dpnba Non-Oxidizing Biocide?
A: When stored properly in its original sealed container, the product maintains stability for 12 months from the date of manufacture.
Q: Can this biocide be used in food or pharmaceutical production applications?
A: This product is for industrial and laboratory research use only. It is not intended for direct contact with food, pharmaceuticals, or medical applications.
Q: What documentation is provided with each order?
A: Each shipment includes a Certificate of Analysis (COA) and Material Safety Data Sheet (MSDS) specific to the batch.
Q: Is custom packaging available beyond the standard 25kg plastic bucket?
A: Yes, we offer custom packaging options for large-volume orders. Contact our sales team to discuss your specific requirements.
Q: How is the bactericidal efficacy of this product verified?
A: Efficacy testing is conducted per industry standards, with results available in the batch-specific COA. Additional third-party testing can be arranged upon request.