
For industrial manufacturing and laboratory research purposes only.
Product Specifications
| Parameter | Value |
|---|---|
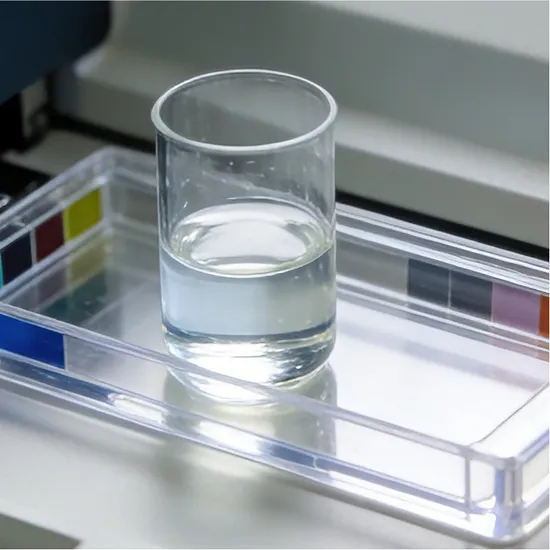
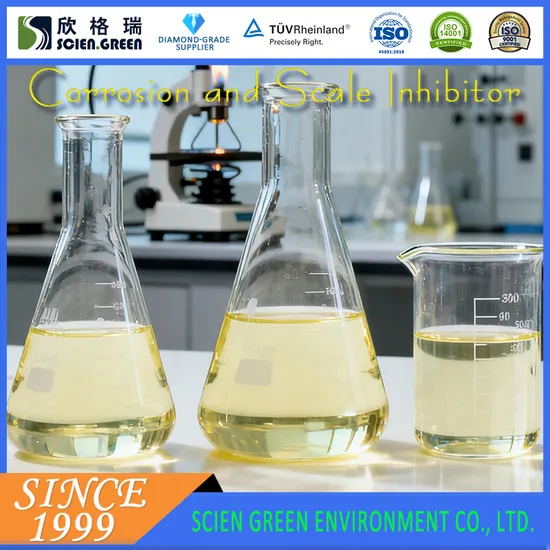
| Color | Pale Yellow Liquid |
| Appearance | Liquid |
| Type | Industrial Circulating Water Treatment Agent |
| Product Name | Scale Corrosion Inhibitor for Chemical Industry |
| Total Phosphate (as Po43-) Content (%) | ≤5.0 |
| a-Zole (as C6h5n3) Content(%) | ≤1.0 |
| Solid Content (%) | ≥28.0 |
| Density (20°C) G/Cm³ | ≥1.13 |
| pH (1% Aqueous Solution) | 1.5-5.0 |
| Shelf Life | 1 Year |
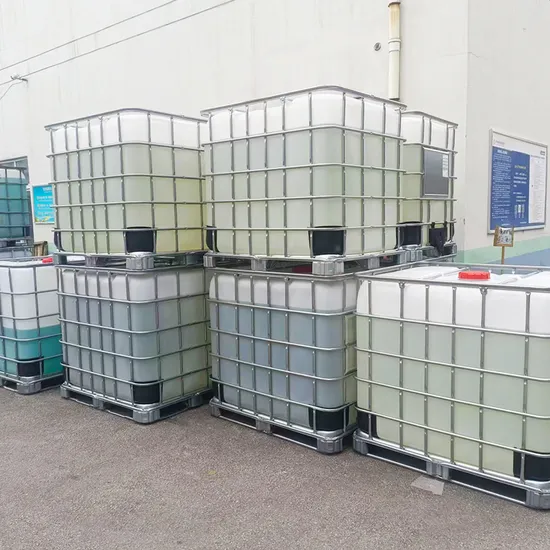
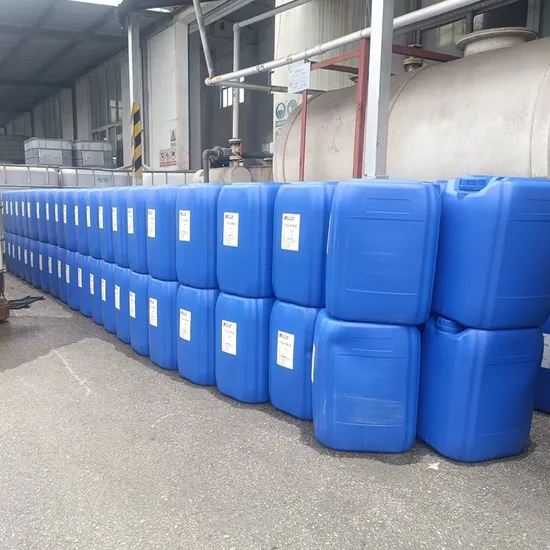
| Transport Package | Blue / White Plastics Drum |
| Specification | 25 kg/200 kg/1 ton drum |
| Trademark | GIDINEW |
| Origin | Jining City, Shandong Province, China |
| Production Capacity | 15000 Ton/Year |
| Package Size | 120.00cm * 100.00cm * 115.00cm |
| Package Gross Weight | 1057.000kg |
Circulating Water Treatment Chemical Scale Corrosion Inhibitor: Solving High Phosphate and Delivery Delays in Chemical Industry
For over a decade, we've witnessed chemical plants struggle with circulating water systems—traditional inhibitors either exceed environmental phosphate limits or fail to prevent scaling during peak production. Research labs face similar frustrations: small-batch orders get deprioritized by large manufacturers, delaying critical R&D trials. These pain points aren't just inconvenient; they directly impact operational efficiency and compliance costs.
Fast-Delivery Circulating Water Treatment Solution for Small-Batch Needs
Our Circulating Water Treatment Chemical Scale Corrosion Inhibitor with ≤5.0% Total Phosphate addresses these challenges head-on. As a specialized provider focusing on small-batch customized synthesis, we guarantee response within 24 hours and delivery of small-batch orders in 7-15 days—perfect for both emergency production line needs and laboratory testing phases. This low phosphate inhibitor maintains strict environmental compliance while delivering reliable scale and corrosion protection.
Industrial Applications in Chemical Manufacturing
This Chemical Industry Scale Corrosion Inhibitor is engineered for closed-loop and open recirculating water systems in chemical processing plants, refineries, and industrial cooling towers. It effectively controls calcium carbonate, calcium sulfate, and phosphate scaling while inhibiting corrosion on carbon steel, copper, and alloy surfaces—critical for maintaining heat exchange efficiency and extending equipment lifespan in high-temperature industrial environments.
Key Specifications and Their Industrial Impact
The ≤5.0% total phosphate content ensures compliance with strict environmental discharge regulations, eliminating the need for costly phosphate removal systems. With a solid content of ≥28.0%, this inhibitor provides concentrated performance, reducing storage and transportation costs compared to dilute alternatives. The density of ≥1.13 g/cm³ at 20°C ensures easy metering and mixing in automated dosing systems, while the pH range of 1.5-5.0 guarantees stability across varying water chemistry conditions. The ≤1.0% a-Zole content provides additional copper corrosion protection, making it suitable for mixed-metal systems common in chemical processing facilities.
Benefits of Low Phosphate Inhibitor for Industrial Operations
Choosing our Low Phosphate Inhibitor translates to quantifiable operational benefits: reduced downtime from scale-related equipment failures, lower chemical consumption due to high active content, and compliance with increasingly stringent environmental regulations. Unlike generic inhibitors, our product's consistent formulation ensures predictable performance, minimizing the risk of unexpected scaling or corrosion events that could halt production. With annual production capacity of 15,000 tons, we provide the stability of large-scale manufacturing with the flexibility of small-batch service.
Quality Assurance You Can Verify
Every batch of our Circulating Water Treatment Chemical undergoes rigorous quality testing, including density measurement, pH analysis, and phosphate content verification. We provide a Certificate of Analysis (COA) with each shipment, detailing all key parameters. Our production facility follows strict quality control protocols, ensuring batch-to-batch consistency critical for industrial process stability. If any parameter fails to meet specifications, we offer unconditional replacement—no questions asked. Our technical support team is available to assist with dosage optimization and system compatibility assessments, drawing on years of experience in chemical water treatment applications.
Certificate of Analysis & Documentation
Each order includes a detailed Certificate of Analysis (COA) specific to the batch, confirming compliance with all stated specifications. Material Safety Data Sheets (MSDS) are provided for safe handling and regulatory compliance. For critical applications, additional testing documentation can be requested, including corrosion rate measurements and scale inhibition efficiency data under simulated operating conditions.
Storage & Handling
- Store in a cool, dry, well-ventilated area, sealed and away from direct sunlight.
- Keep away from incompatible materials, food and feed sources.
- Handle with appropriate personal protective equipment (gloves, goggles, lab coat).
- Follow good industrial hygiene practices. Avoid inhalation and skin contact.
- Refer to MSDS for detailed storage and safety instructions.
Streamlined Order Process for Industrial and Laboratory Needs
Our ordering process is designed for efficiency: submit your requirements via phone or email, receive a detailed quote within 24 hours, confirm specifications, and schedule delivery. We offer flexible packaging from 25 kg drums for laboratory trials to 1-ton containers for production-scale applications. All shipments include the necessary documentation for regulatory compliance, and our logistics partners ensure on-time delivery to your facility.
Frequently Asked Questions
Q: What is the shelf life of this scale corrosion inhibitor?
A: The product has a shelf life of 1 year when stored in a sealed container under recommended conditions.
Q: Can this product be used in food or pharmaceutical applications?
A: No, this product is for industrial and laboratory research use only, not for direct human consumption or therapeutic applications.
Q: What documentation is provided with each order?
A: Each shipment includes a Certificate of Analysis (COA) and Material Safety Data Sheet (MSDS).
Q: Are custom packaging sizes available?
A: Standard packaging includes 25 kg, 200 kg, and 1-ton drums; custom packaging may be available for large-volume orders.
Q: How is the phosphate content controlled during production?
A: Our manufacturing process includes in-line phosphate monitoring and final batch testing to ensure total phosphate content remains ≤5.0% as specified.